
Soorty’s vertical model was built for denim. At Nooriabad it now runs a woven mill as well, producing one million yards a month of non-denim fabric, PFD or mill-dyed, from greige through to graded roll.
CAPACITY
What the mill runs, and what
has been approved
Approved investment is listed separately from installed capacity, and dated wherever the
programme sets a date.
CURRENT installed and running
PLANNED approved, not yet operational
1M yd
Woven fabric per month, PFD and mill-dyed
Nooriabad non-denim mill, commissioned 2024
1.7M yd
Per month following the piece-dyed mill expansion
Adds bleaching range and stenter capacity
Adds bleaching range and stenter capacity
2024
Mill commissioned.Weaving, pre-treatment, dyeing, finishing and grading on one site
No external conversion step between greige fabric and graded roll
400,00Om
Per month of digital textile printing at the non-denim mill
Within Soorty's $40 million group investment programme
PRODUCT
Eight fabric families out of one mill, from shirting to bottomweight canvas.
Fabric families
Twills, canvas, poplin, Oxford, chambray and dobby structures, in cotton, cellulosic, linen and synthetic blends. The range is built around the constructions apparel programmes keep coming back to.
Bottom wear
Cotton twills, stretch twills, nylon/cotton, linen/cotton blends, canvas
Casual and fashion twills
Cotton/poly, cotton/nylon, TENCEL™ twill
Workwear and utility
Nylon/cotton, polyester/cotton, canvas, FR fabrics
Shirting
Nylon/cotton, polyester/cotton, canvas, FR fabrics
Linen and natural blends
Linen/cotton blends across bottom-weight and shirting constructions
Performance and activewear
Nylon and polyester blends, stretch and moisture-management fabrics; lightweight stretch, nylon/poly and recycled polyester blends
Sustainable and recycled
Organic cotton, recycled cotton, recycled polyester, TENCEL™M, REFIBRA™M
Dobby design
Dobby structures, herringbone, broken twill, rib structures
INTEGRATED PROCESS CHAIN
Greige to graded roll, on one site
Weaving, preparation, colour and finish sit under one roof at Nooriabad. Nothing leaves the site for an outside processor, which gives the development and production teams tighter control of shade, hand and continuity between lots, and takes a set of hand-offs out of the schedule.
01
Weaving
Air-jet and rapier
looms.
40,000-45,000 m
PER DAY
02
Pre-treatment
Singeing, desizing. mercerising
35,000–40,000 m
PER DAY
03
Dyeing
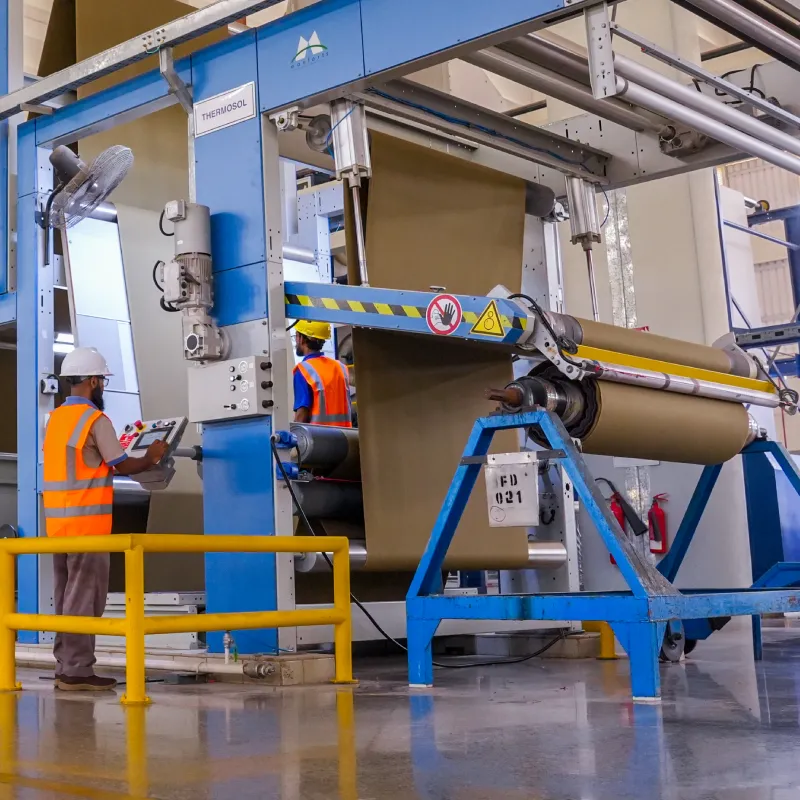
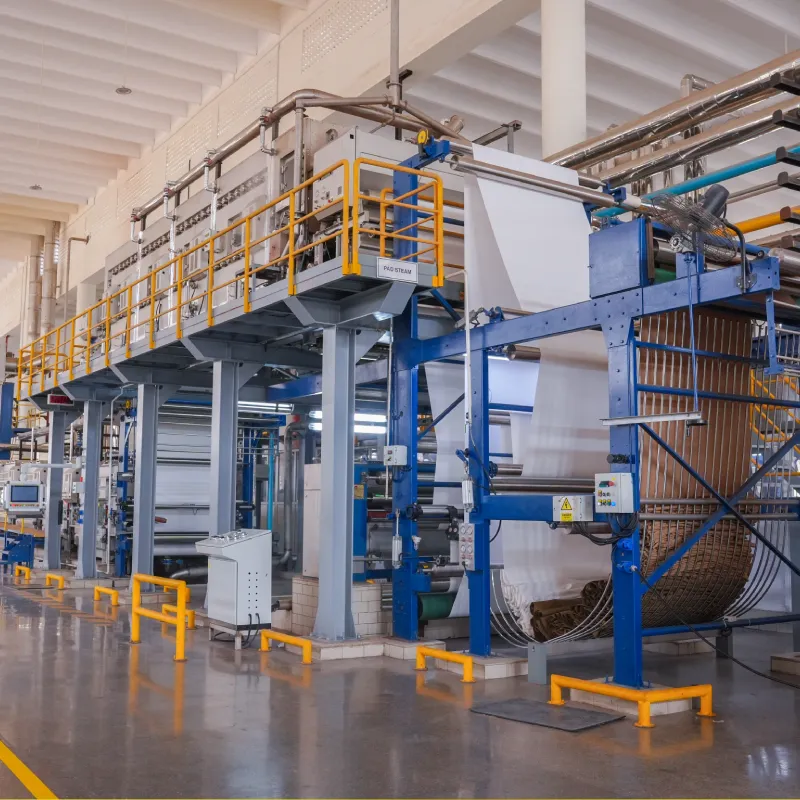
Cold pad batch, thermosol, pad steam, jigger.
30,000-35,000 m
PER DAY
04
Finishing
Stenter, sanforising, sueding.
30,000-35,000 m
PER DAY
05
Grading
Inspection and
packing.
35,000–40,000 m
PER DAY
Daily figures are installed capability per process. Monthly output depends on the construction, the shade and the route a quality takes through the chain.
01. WEAVING
Two loom types on the floor
Air-jet looms run fast and hold a repeat well, which suits
plain and twill constructions in volume. Rapier looms take the heavier and less uniform yarns, and the weft sequencing behind dobby structures, herringbone, broken twill and rib patterns.
Having both at Nooriabad widens what the millcan put into development: more constructions, a broader yarn range, heavier and lighter weights, more complicated patterning.
02- PRE-TREATMENT
Preparation decides the shade
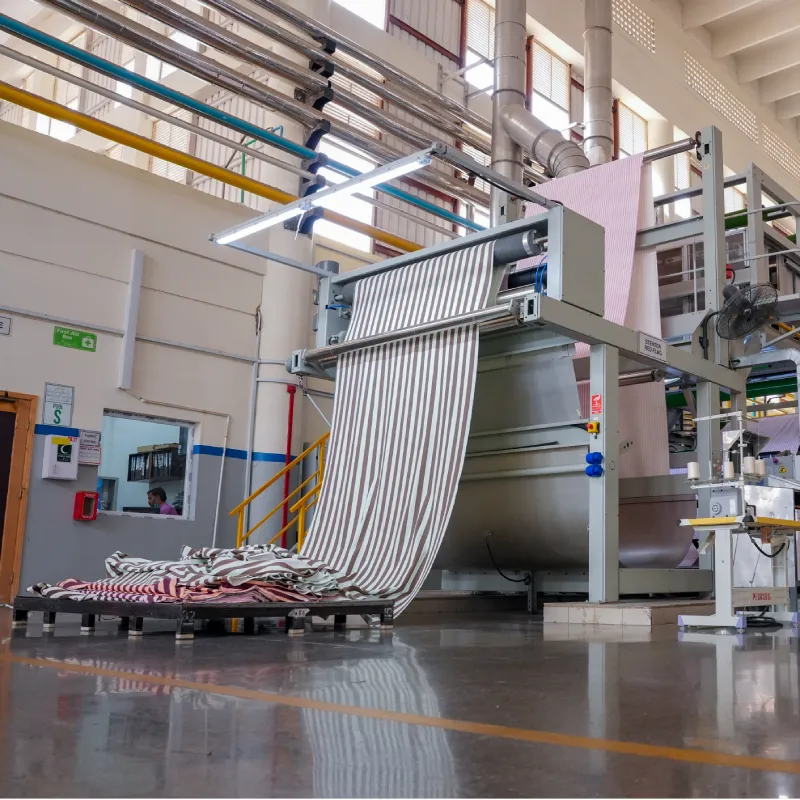
Singeing, desizing, mercerising and bleaching all run inhouse, on Osthoff-Senge, Benninger and RedFlag plant. Preparation sets absorbency, whiteness and surface. Get it even across the width and a shade will reproduce from lab dip through to bulk; get it wrong and no amount of dyehouse work recovers it.
Mercerising adds lustre, strength and dye uptake. Bleach
white and optical bright are finished qualities here in their
own right, not only a step on the way to a colour.
03. COLOUR AND FINISH
Four dyeing routes under one roof
Fibre and shade depth dictate the chemistry. A pale cotton
poplin and a deep polyester-rich twill want different things
from a dyehouse. Cold pad batch, pad thermosol, pad steam and high-temperature jigger are all installed here, so a quality can be developed around what it is made of and what it has to do.
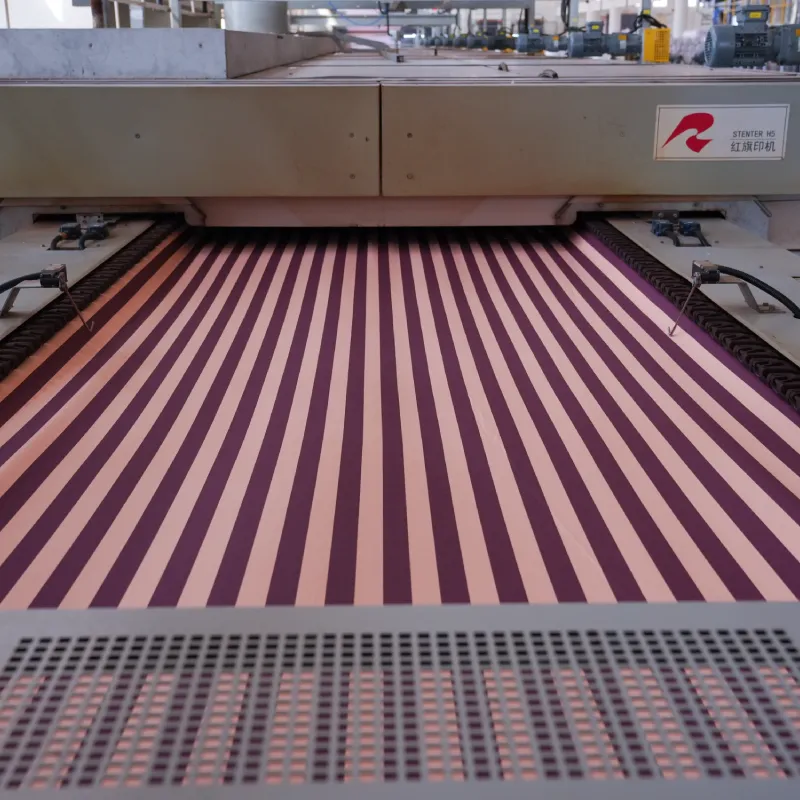
Finishing follows on stenter, sanforising and Lafer Microsand
Diamond sueding. This is the stage that fixes width and
shrinkage, and where a flat fabric becomes a peached or
sueded one.
THE PLANT
What a quality passes through between greige and graded roll.
Dye routes, dye classes, finishes
All of it in-house at Nooriabad, with the machine and its daily capacity against each route.
DYEING ROUTES
Cold pad batch
Benninger 32,000 m/day
Pad thermosol
Monforts 42,000 m/day
Pad steam
RedFlag 45,000 m/day
High-temperature jigger
GoldMine -7,000 m/day
DYE CLASSES
Reactive
Vat
Disperse /reactive
Disperse/vat
Pigment
Sulphur
Indigo
FINISHES
Stenter
RedFlag 45,000 m/day
Sanforising
Monforts 42,000 m/day
Microsand Diamond sueding
Lafer 24,000 m/day
Bleach white and optical brighT
RedFlag bleaching -54,000 m/day
Installed plant
Six suppliers between them carry the chain. Capacities are
per machine line, per day.
Osthoff-Senge
Benninger
Monforts
RedFlag
GoldMine
Lafer
Singeing and desizing
Mercerising; cold pad batch dyeing
Pad thermosol dyeing; sanforising
Bleaching stenter; pad steam dyeing
High-temperature jigger dyeing
Microsand Diamond sueding
60,000 m/day
65,000 m/day mercerising 32,000 m/day
cold pad batch
42,000 m/day pad thermosol -45,000 m/day
sanforising
54,000 m/day bleachingl 45,000 m/day stenter
45,00О
m/day pad steam
7,000 m/day
24,000 m/day
Osthoff-Senge
Benninger
Monforts
RedFlag
GoldMine
Lafer
Singeing and desizing
Mercerising; cold pad batch dyeing
Pad thermosol dyeing; sanforising
Bleaching stenter; pad steam dyeing
High-temperature jigger dyeing
Microsand Diamond sueding
60,000 m/day
65,000 m/day mercerising 32,000 m/day
cold pad batch
42,000 m/day pad thermosol -45,000 m/day sanforising
54,000 m/day bleachingl 45,000 m/day stenter 45,00О m/day pad steam
7,000 m/day
24,000 m/day
Osthoff-Senge
Singeing and desizing
60,000 m/day
Benninger
Mercerising; cold pad batch dyeing
65,000 m/day mercerising 32,000 m/day cold pad batch
Monforts
Pad thermosol dyeing; sanforising
42,000 m/day pad thermosol -45,000 m/day sanforising
RedFlag
Bleaching stenter; pad steam dyeing
54,000 m/day bleachingl 45,000 m/day stenter 45,00О m/day pad steam
GoldMine
High-temperature jigger dyeing
7,000 m/day
Lafer
Microsand Diamond sueding
24,000 m/day
Who checks the fabric, and where
The non-denim mill has its own laboratory. Behind it sit the
wider Nooriabad site’s laboratories and Soorty’s group
quality systems, which keep inspection and release separate
from the people running production.
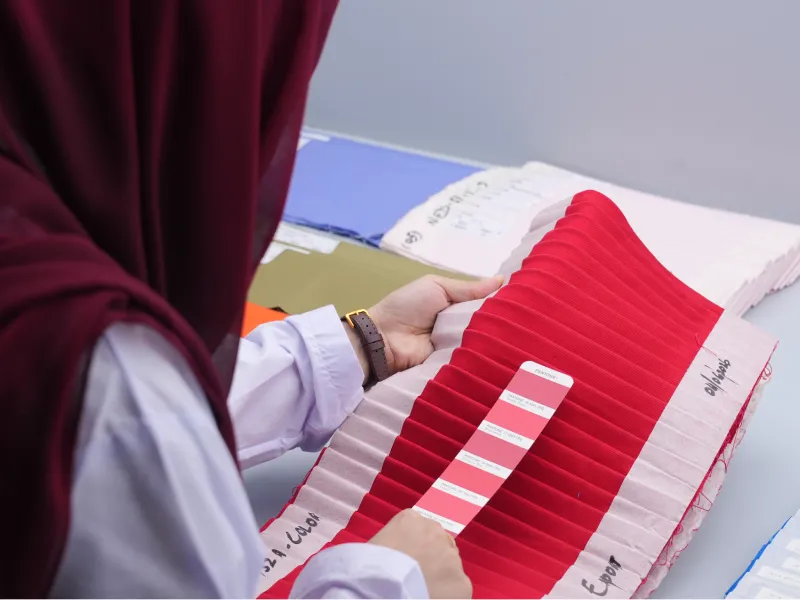
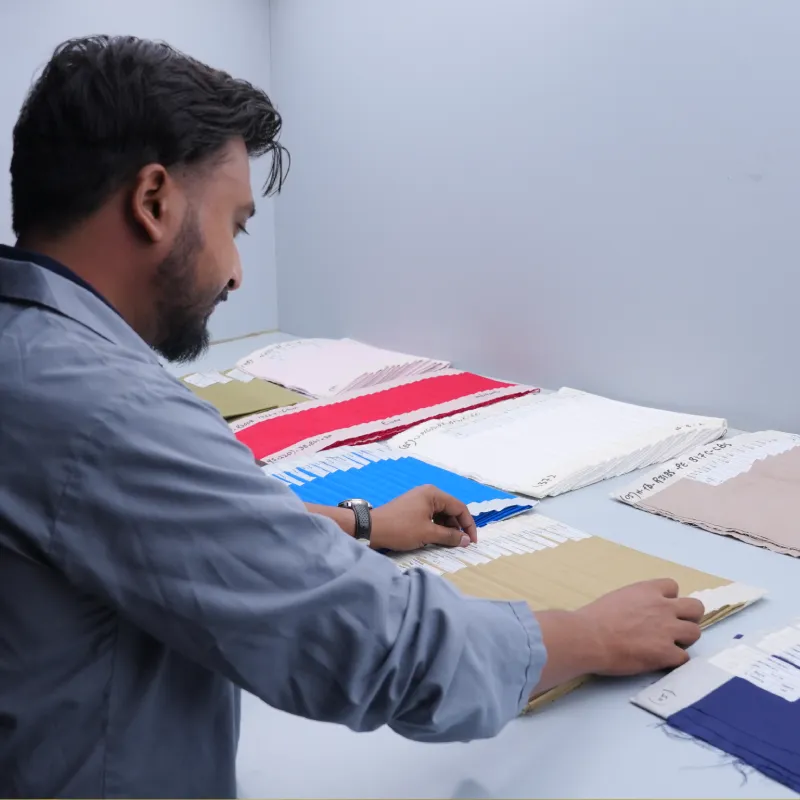
Shade assessment against standard. Non-denim mill, Nooriabad.
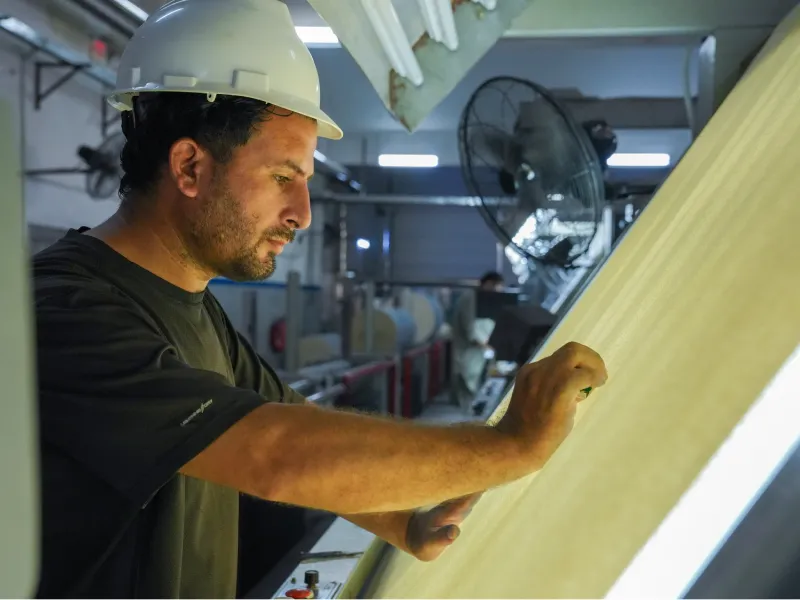
Inspection and grading before packing, at 35,000 to 40,000 m a day.
Non-denim mill laboratory
AT THE MILL
Shade, strength, recovery and fastness, tested on site at Nooriabad. Development yardage and bulk are measured against the same parameters.
Nooriabad site laboratories
UNIT 13. WIDER SITE
Unit 13 also houses Soorty’s spinning and denim operations. Its in-house laboratory infrastructure carries buyer approvals including Levi Strauss & Co., Gap, JCPenney and Spanx.
Group quality systems
SOORTY GROUP
Real Time Quality, Soorty’s own application, records internal check points as they happen across Pakistan and Bangladesh, with Power Bl behind it for trend and root-cause work. Shipments are released by an independent Quality Inspection Department, and a separate Process Control Department checks that processes are being run as specified. In Pakistan, Quality Assurance reports to the Deputy Managing Director, not to production.
VERTICAL CONNECTION
Not a standalone fabric mill
Soorty spins its own yarn, develops product from cotton
seed onwards, and sews in Pakistan and Bangladesh. A
woven programme can therefore keep fibre, yarn, fabric and garment inside one supplier relationship.
Non-denim woven bottoms and shirts are made in Karachi
and Cumilla, and non-denim woven casual bottoms are an
established product at Soorty Textiles Bangladesh.
From fibre to finished garment
Every step here is a Soorty operation, not a nominated
supplier.Which fibres and yarn technologies suit a
particular woven construction gets settled in development.
FIBRE AND YARN
Spinning
SOORTY GROUP
Rieter and Toyota ring spinning. The group fibre portfolio spans cotton. ELS and Pima, linen and European Flax, hemp, TENCEL ™ Lyocell and Modal, LENZING™M ECOVERO™M Circulose®, COOLMAX®, and recycled polyester and nylon,with LYCRA® and core-spun stretch yarns.
DEVELOPMENT
R&D and design
SOORTY GROUP
Product development and R&D leadership in Karachi, with design studios in Barcelona, Amsterdam, London and New York. The Soorty Digital Library has held the fabric and trend archive online since 2020.
FABRIC
Nooriabad
THIS MILL
Weaving, pre-treatment, dyeing. finishing and grading, alongside the group's spinning and denim operations on the same site.
GARMENT
Karachi and Cumilla
SOORTY GARMENTS
Non-denim woven bottoms and shirts, with laundry, embroidery, in-house laboratories and buyerapproved inspection in both countries.
WHAT IS NEXT
Committed
Two approved investments will extend what the mill can produce. A third is renewable energy.
Digital textile printing, 400,000 m a month. It sits inside Soorty’s $40 million group investment programme, which also funds digital denim printing, all-over printing and direct-to-garment printing elsewhere in the group.
Piece-dyed mill expansion to 1.7 million yards a month. It
adds bleaching range and stenter capacity. More stenter time widens what can be developed, not only what can be produced.
WORKING WITH US
Start at development, not at the order
Construction, yarn, loom, dye route, finish and laboratory all sit inside Soorty, with the garment factories behind them. Bring a woven quality to the mill while it is still open and more of that range is available to it. Bring it as a closed specification and most of the decisions have already been made somewhere else.
A kinder version of denim.
CONTACT US
- Plot 26, Sector 23, Korangi Industrial Area, Karachi 74900, Pakistan
- +92 21 38709084
- contactus@soorty.com
FOLLOW US
Linkedln • Instagram • Facebook • YouTube